SYSTEMATIC SURFACE FINISHING
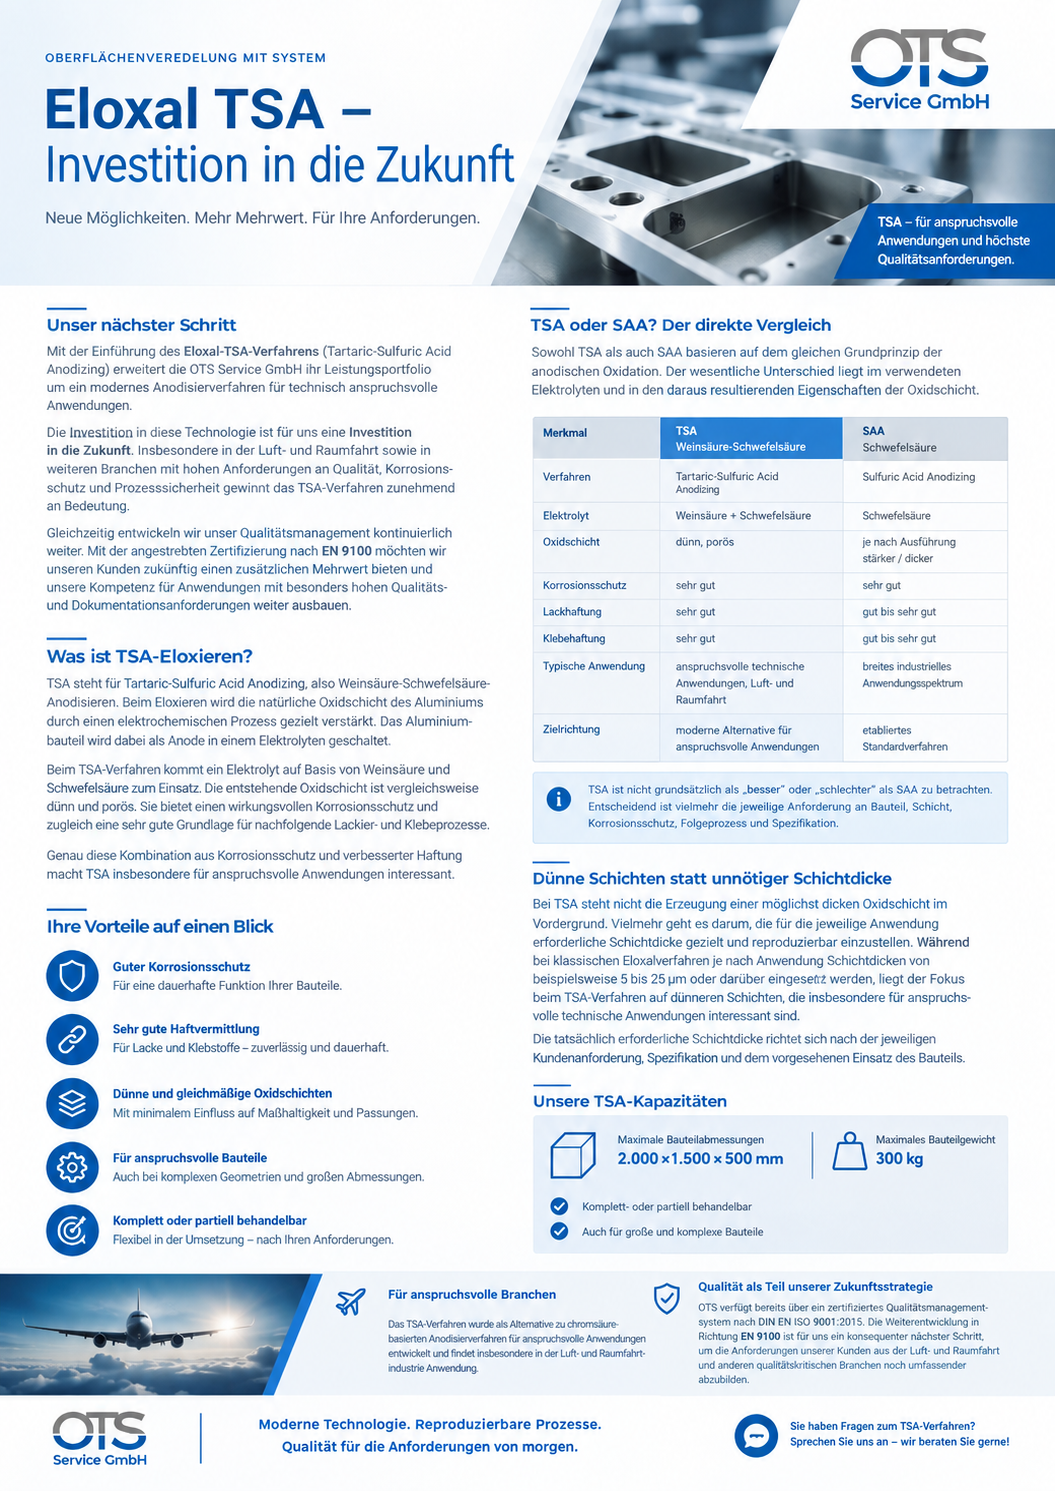
Eloxal TSA—An Investment in the Future
New possibilities. Greater value. Tailored to your needs.
Our Next Step
With the introduction of the Eloxal-TSA process (Tartaric-Sulfuric Acid Anodizing), OTS Service GmbH is expanding its service portfolio to include a modern anodizing process for technically demanding applications.
For us, investing in this technology is an investment in the future. The TSA process is becoming increasingly important, particularly in the aerospace industry and other sectors with high demands on quality, corrosion protection, and process reliability.
At the same time, we are continuously refining our quality management system. By pursuing certification under EN 9100, we aim to offer our customers additional value in the future and further expand our expertise for applications with particularly high quality and documentation requirements.
What Is TSA Anodizing?
TSA stands for Tartaric-Sulfuric Acid Anodizing. In the anodizing process, the natural oxide layer of aluminum is selectively strengthened through an electrochemical process. The aluminum component is connected as an anode in an electrolyte.
The TSA process uses an electrolyte based on tartaric acid and sulfuric acid. The resulting oxide layer is relatively thin and porous. It provides effective corrosion protection and, at the same time, serves as an excellent foundation for subsequent painting and bonding processes.
It is precisely this combination of corrosion protection and improved adhesion that makes TSA particularly suitable for demanding applications.
Your Benefits at a Glance
Excellent corrosion protection
To ensure the long-term functionality of your components.
Excellent adhesion promotion
For paints and adhesives—reliable and durable.
Thin and uniform oxide layers
With minimal impact on dimensional accuracy and fits.
For demanding components
Even with complex geometries and large dimensions.
Can be treated completely or partially
Flexible implementation—tailored to your requirements.
TSA or SAA? A Direct Comparison
Both TSA and SAA are based on the same fundamental principle of anodic oxidation. The main difference lies in the electrolyte used and the resulting properties of the oxide layer.
| Characteristic | TSA Tartaric-Sulfuric Acid Characteristic |
SAA Sulfuric acid |
| Procedure | Tartaric-Sulfuric Acid Anodizing |
Sulfuric Acid Anodizing |
| Elektrolyte | Tartaric Acid + Sulfuric Acid | Sulfuric Acid |
| Oxide layer | thin, porous | stronger/thicker, depending on the model |
| Corrosion Protection | very good | very good |
| Paint Adhesion | very good | good to very good |
| Adhesive Bond Strength | very good | good to very good |
| Typical Application | Demanding technical applications, aerospace | wide range of industrial applications |
| Direction | A modern alternative for demanding applications | established standard procedure |
TSA should not generally be considered “better” or “worse” than SAA.Rather, the decisive factors are the specific requirements for the component, coating, corrosion protection, subsequent process, and specifications.
Thin layers instead of unnecessary layer thicknesse
With TSA, the focus is not on producing the thickest possible oxide layer. Rather, the goal is to precisely and reproducibly adjust the layer thickness required for the specific application. While conventional anodizing processes use layer thicknesses ranging from, for example, 5 to 25 µm or more depending on the application, the TSA process focuses on thinner layers, which are particularly useful for demanding technical applications.
The actual layer thickness required depends on the customer’s specific requirements, specifications, and the intended use of the component.
Our TSA Capabilities
- Maximum component dimensions: 2,000 x 1,500 x 500 mm
- Maximum component weight: 300 kg
- Can be treated completely or partially
- Even for large and complex components